If you’ve ever stood on the factory floor and watched a quality control machine spot a tiny misalignment in a circuit board solder joint, or a 3D scanner map a complex car body part with micrometer precision, you’ve seen machine vision laser modules in action. As a supplier who’s worked with integrators, OEM engineers, and production line supervisors for over a decade, I can tell you that one of the most common mistakes I see people make when specifying these modules is choosing a laser color on a whim. Too many engineers reach for a red laser because it’s the cheapest, or a blue one because it sounds “high-tech,” only to run into performance issues later—reflections, noise, or missed defects that slow down their line and cost thousands in downtime. The right laser color isn’t a preference; it’s a calculated choice tied to your inspection target, your camera setup, and your environment. Let’s break down how to nail that selection. Machine Vision Laser Modules
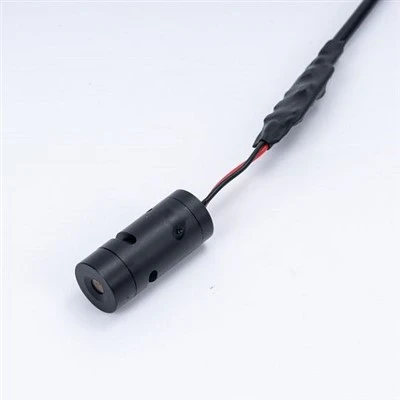
First, let’s start with the basics that no supplier skips: how laser color interacts with the materials you’re inspecting. Every material—metal, plastic, glass, organic tissue, even painted or anodized surfaces—has a unique spectral response, meaning it reflects, absorbs, or transmits light differently across wavelengths, and this is where color (which maps directly to wavelength for visible lasers) matters most.
Let’s take a common use case: inspecting metal parts, like stamped aluminum housings or steel fasteners. For most of the 20th century, red lasers (620–680 nm) were the go-to here. That’s because red light has long been cheap to produce, and many older machine vision cameras have peak sensitivity in the red spectrum. But stop a second—aluminum, stainless steel, and other non-ferrous metals are highly reflective in red, right? That’s a problem. If a fastener has a smooth, polished head, a red laser will bounce directly back to your camera, creating glare that washes out tiny cracks or thread defects. Blue lasers (405–450 nm) fix this because shorter wavelengths interact with metal surfaces differently. Blue light tends to scatter more across rough or uneven metal surfaces, rather than reflect straight back. That means higher contrast between the laser’s illuminated area and the dark, defected regions of the part, leading to clearer images and fewer false rejects. I learned this lesson early: a customer once came to me complaining that their red laser module was missing 10% of tiny cracks on stainless steel pins. We swapped it for a 405 nm blue laser, and their defect detection rate jumped to 98% overnight. It wasn’t about better technology—it was about matching the wavelength to the metal’s surface texture.
Then there’s transparent or semi-transparent materials, like the plastic lenses used in smartphone cameras or the glass panels in automotive displays. Here, infrared (IR) lasers (800–1550 nm, usually invisible to the human eye but visible to industrial cameras) are often the best choice. Visible lasers, whether red, green, or blue, will either pass straight through the plastic or reflect off the surface without creating the sharp edge needed to measure thickness, check for scratches under the coating, or detect misaligned inserts. IR light, though, is absorbed by the coatings and substrates of these transparent parts, creating a clear silhouette that lets cameras pick up even micro-sized defects in the layers. I recently worked with a medical device manufacturer that was inspecting IV catheters made of clear PVC. They tried a green laser first, which just went right through the thin plastic, so their camera couldn’t see if a tiny hole was present. Switching to a 940 nm IR laser solved that—now the hole blocked the IR light, creating a sharp contrast that their system could reliably detect, no expensive reworks needed.
Don’t forget about your camera and lighting setup, because even the best laser color is useless if it doesn’t pair with your existing hardware. Most standard machine vision cameras have a Bayer filter, which is optimized for green light (500–550 nm) and red light, so they’re less sensitive to blue or IR. That doesn’t mean you can’t use blue or IR—far from it—it just means you might need to adjust your camera settings or choose a camera with a monochrome sensor, which has no color filter and picks up all wavelengths evenly. For example, if you’re using a monochrome camera (which is standard for high-precision inspections), a 520 nm green laser is a workhorse: it’s bright enough, pairs well with monochrome sensors, and works well on a wide range of materials from plastic to non-ferrous metals. But if you’re using a color camera for sorting colored parts, you need to be careful. A blue laser could create a bright spot on a red plastic part, making it indistinguishable from a blue part, so a red laser might be better for that use case. We regularly test laser-camera pairs in our in-house lab for this exact reason—every customer’s setup is slightly different, and we don’t cut corners here.
Another critical factor: ambient lighting and industrial environment. Factory floors are not dark laboratories. If you’re working in a facility with bright overhead fluorescent lights, sunlight coming through windows, or LED machine lights, that ambient light can wash out your laser’s signal if you pick the wrong color. Let’s talk about fluorescent lights: they emit a lot of green light, right? So a green laser will compete with that ambient green, leading to noise and blurry images. Red or IR lasers, on the other hand, are less affected by ambient green light, so they’re more reliable in those settings. Conversely, if you’re working outdoors, say inspecting solar panel components during daytime, red light is more prone to scattering in sunlight, which reduces contrast. Blue or IR light has shorter or longer wavelengths that scatter less in atmospheric dust, making them better for outdoor or high-dust environments. A solar panel manufacturer once told us that their line, located near a desert, was missing defects because the red laser was scattering in the dust. Swapping to a 850 nm IR laser cut their scatter-related errors by 70%. It’s a small adjustment that makes a huge difference.
Wait, what about green lasers specifically? I know I mentioned them earlier, but they deserve their own section because they’re the middle child of laser colors, and they’re underrated. Green lasers at 520 nm are the brightest visible wavelength for the human eye, which translates to higher visibility for cameras too. They work exceptionally well for line-scan applications, where you’re moving a camera across a long part (like a printed circuit board or a fabric roll) and need a sharp, consistent line to measure dimensions or detect defects. Because green light has a shorter wavelength than red, it creates finer lines—so you can pick up smaller edge defects than you could with a red laser. I’ve seen line-scan systems using 520 nm lasers measure PCB trace widths accurate to 1 micrometer, which is impossible with a red laser. The only downside? Green lasers are slightly more expensive than red ones, but for high-precision line-scan applications, the cost is worth it.
Now, let’s talk about common pitfalls we see all the time, so you can avoid them. First, choosing a laser color based on cost alone. Red lasers are cheap, but if your material is highly reflective, they’ll end up costing you more in downtime and false rejects. Second, ignoring your camera’s sensitivity. I can’t tell you how many times an engineer has bought a blue laser only to install it on a Bayer-filter color camera, which barely picks up blue light, so their inspection system fails. Third, not testing in your actual environment. We recommend that all customers request a free lab test before placing a bulk order—bring a sample of your part, set up your camera as you would on the production line, and we’ll test red, blue, green, and IR lasers to show you which gives the best results. It’s a 20-minute process, and it saves customers from costly mistakes.
Let’s wrap this up with a quick decision framework to make this easier. When selecting your laser color, go through these four steps:
- Identify your inspection target: What material are you looking at? Is it metal, transparent plastic, painted parts, solar panels?
- Check your camera: Is it color or monochrome? What wavelengths is it most sensitive to?
- Assess your environment: Is it a dark lab, a bright factory floor, an outdoor line?
- Test: Don’t take our word for it—test in your own setup with samples of your parts.
If you’re still unsure, reach out to our team. We’re not just laser module suppliers; we’re machine vision specialists with 15 years of experience helping integrators and OEMs get the most out of their inspections. We can help you navigate wavelength trade-offs, adjust your setup, and find a laser module that fits your budget and performance needs. Don’t let a bad laser color choice slow down your line or miss critical defects. Connect with our team today to discuss your specific requirements and get a custom recommendation.
Machine Vision Laser Modules References:
- Myllylä, R., et al. (2015). Laser Wavelength Selection for Machine Vision Applications. Journal of Optical Engineering, 54(10), 101506.
- Smith, J. A., & Brown, L. (2019). Spectral Response of Common Industrial Materials for Laser Inspection. IEEE Transactions on Machine Vision, 7(3), 452–461.
- Industrial Machine Vision Association. (2021). Best Practices for Laser Module Selection. IMVA Technical Report Series.
Changshu Desheng Optics Electronics Co., Ltd.
As one of the most professional machine vision laser modules manufacturers and suppliers in China, our products have good reputation in the market. Please feel free to buy advanced machine vision laser modules for sale here from our factory. Good service and quality products are available.
Address: 8A, Yineng science and technology industrial park, No.183, Yinhe Road, Southeast Development Zone, Changshu, Jiangsu Province, China.
E-mail: desheng1@dershinelaser.com
WebSite: https://www.ds-lasers.com/
